Pipe systems for the chemical industry:
reliable, efficient and safe to use

Advantages of PE pipe systems for applications in the chemical industry
Some applications in industry require permanent monitoring for potential leaks in order to protect the environment, and possibly also to comply with legal requirements. This reliably prevents chemical media from escaping into the environment, potential consequential damage to people and nature, and the resulting liability risks.
Source: Sustainability

Properties of PE pipe systems for the chemical industry

Corrosion resistance
Corrosion causes annual damage amounting to 3% of the gross national product (Source: WCO World Corrosion Organisation). Plastic pipe systems do not corrode and exhibit high resistance to aggressive media. Therefore, they offer high operational safety, are robust, and yet flexible.
Flexibility
The high flexibility of the polyethylene material enables handling and transport of long coiled lengths in ring coils or from a drum. This makes polyethylene pipes ideal for renewal by pulling them into the old pipe. A special renewal option is the use of pre-deformed pipes, which enable trenchless insertion of long lengths even in dimensions up to 500 mm and, during subsequent operation, fit close to the old pipe (close-fit).
Permanently tight welded connections
Polyethylene can be welded easily and safely. The specifications are well-established and described in the DVS regulations. The resulting connections are tension-resistant and permanently leak-tight. They thus enable the safe operation of pressure lines even for sensitive or hazardous media.
Permeation resistance
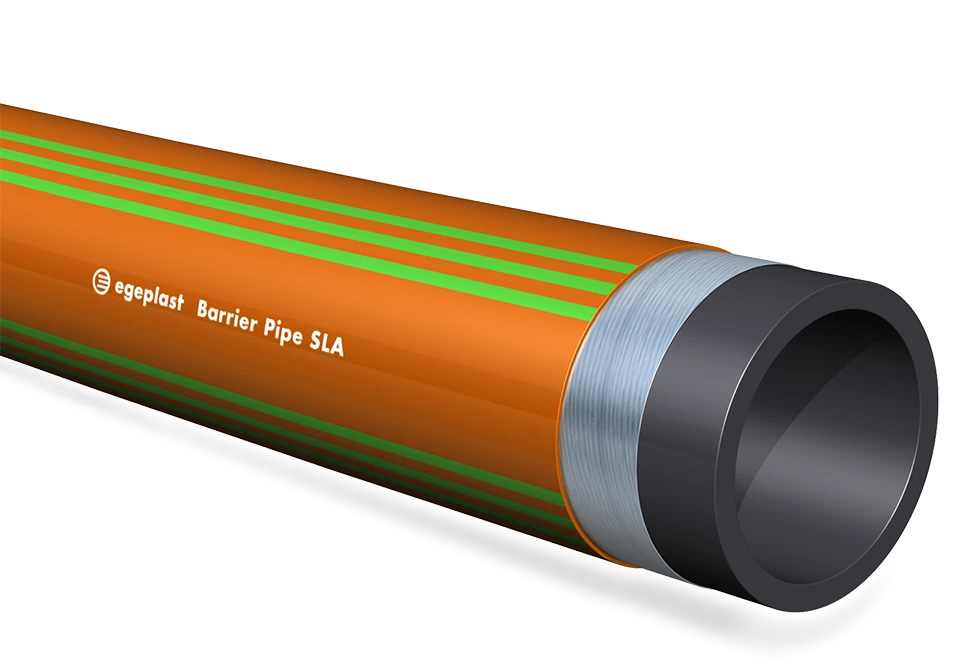
Plastic pipes are resistant to most chemicals and also hydrocarbons. However, permeation can occur, especially with hydrocarbons. Plastic pipes with barrier layers are therefore ideal for applications that require a permeation-resistant pipe system. A permeation barrier layer reliably prevents pollutants from permeating through the pipe wall in both directions.
100% safety through leak monitoring
Some industrial applications require permanent monitoring for potential leaks to protect the environment and possibly comply with legal requirements. The escape of chemical media into the environment, potential consequential damage to humans and nature, and the resulting liability risks can thus be reliably excluded. An electrically conductive aluminum layer integrated into the plastic pipe enables 100% leak monitoring for soil and water protection.
Source: Sustainability